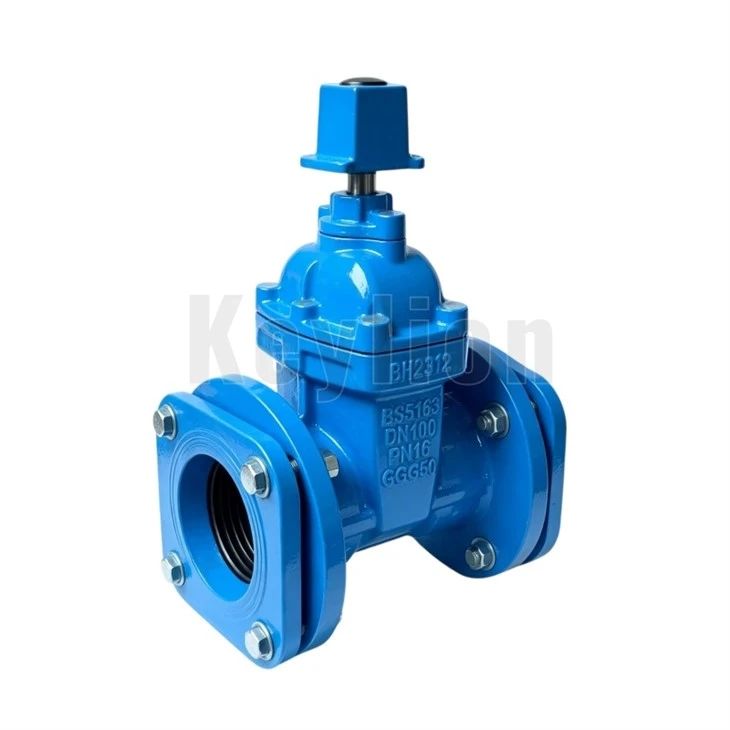

The Underground Non-Rising Stem Gate Valve is engineered for subterranean pipeline networks in municipal water supply, wastewater infrastructure, and fire protection systems. Featuring a compact non-rising stem design, the valve spindle rotates internally without raising the handwheel or operating nut, minimizing required installation space in confined chambers or direct-burial environments.
Built with a fully vulcanized EPDM/NBR resilient wedge and fusion-bonded epoxy coating, this valve provides bubble-tight shutoff (Zero Leakage, Rate A under ISO 5208) and withstands aggressive soil conditions. Direct burial capability eliminates the need for expensive valve chambers when paired with an appropriate telescopic extension spindle and surface cap.
Technical Specifications
|
Parameter |
Specification Details |
|
Size Range |
DN50 to DN1200 (2 inches to 48 inches) |
|
Pressure Rating |
PN10, PN16, PN25 (AWWA Class 125/150 available) |
|
Working Temperature |
-10 deg C to +80 deg C (Potable Water) |
|
Design Standards |
EN 1074-1/-2, EN 1171, AWWA C515 |
|
Face-to-Face |
EN 558 Series 14 / ISO 5752 Series 14 (DIN 3202 F4 / AWWA C509/C515 options) |
|
Flange Drilling |
EN 1092-2 (ISO 7005-2), ASME B16.42 Class 150 |
|
Operation |
Square Operating Nut (for T-key / extension spindle), Handwheel, Spur/Bevel Gearbox |
Key Features
Resilient Seated Wedge: Ductile iron core (EN-GJS-500-7) fully vulcanized with high-grade EPDM. Delivers memory elasticity and bubble-tight sealing, even after extended operation cycles.
Non-Rising Stem Architecture: Precision rolled-thread stem (AISI 420 / ASTM Grade 316) operates entirely internally, preventing thread exposure to groundwater and reducing operational torque over deep burials.
Triple O-Ring Stem Sealing: Upper O-rings prevent external soil/moisture ingress, while lower O-rings are field-serviceable under full system pressure (no system shutdown required for seal inspections).
Smooth Full Bore: Unobstructed, full-flow waterway matches the inner diameter of the pipeline, preventing sediment accumulation and minimizing pressure drop.
Corrosion Protection: Internal and external surfaces coated with Fusion Bonded Epoxy (FBE) powder, min. 250 um thickness, applied via electrostatic fluidized bed process in compliance with DIN 30677-2.
Applications
Municipal Water Distribution: Main transmission lines and regional potable water grids.
Underground Fire Protection Loops: Buried hydrant supply lines demanding high structural reliability and low torque actuation.
Wastewater & Sewage Networks: Gravity and pressure sewer systems requiring chemical resistance against corrosive effluents.
District Cooling & Subterranean Irrigation: Long-term buried fluid transfer loops.
Manufacturing Capability & Customization
Manufacturing operations utilize automated resin-sand molding lines for ductile iron components, ensuring consistent wall thickness and internal surface smoothness. CNC vertical machining centers perform precision boring of body seats and bonnet alignments to eliminate assembly tolerances.
[Factory Visual Cue: Automated resin-sand molding line and CNC seat-machining stations]
Customization Options:
Stem Materials: Upgrade from standard AISI 420 to AISI 316 / ASTM Grade 316 for high-salinity or acidic soil conditions.
Coating Compliance: WRAS and NSF-61 certified epoxy formulations for strict potable water projects.
Accessories Integration: Factory-fitted ISO 5210 actuator mounting flanges, electric actuators, or telescopic extension spindles sized to specific burial depths (1.5m to 5.0m).
Testing, Quality & Documentation
Every production valve undergoes factory hydrostatic and pneumatic testing in accordance with EN 12266-1 and ISO 5208:
Shell Strength Test: Conducted at 1.5 x PN using water.
Seat Tightness Test: Conducted at 1.1 x PN (high pressure) and low-pressure air testing (0.6 MPa) to verify zero leakage.
Coating Test: High-voltage spark testing (25 kV) to detect pinholes in the epoxy layer.
Traceability & Documentation Supplied:
Material Test Certificates (EN 10204 3.1)
Individual valve hydro-test reports linked by serial number
Coating thickness and adhesion test logs
Installation, Operation, and Maintenance (IOM) Manual
FAQ
Q: Can this valve be buried directly without a concrete valve box?
A: Yes. When paired with a heavy-duty telescopic extension spindle and a surface valve box, the valve body can be buried directly in the backfill trench.
Q: What is the certification status for potable water contact?
A: All internal elastomeric components and epoxy coatings comply with international drinking water standards, including WRAS and NSF-61 requirements depending on client specification.
Q: Are spare parts such as stem O-rings replaceable on-site?
A: Yes. The upper O-ring packing can be safely replaced by removing the retaining clip/gland without excavating the valve body or interrupting pipeline pressure.
Request a Quote
Submit your project specifications below to receive a formal technical proposal, commercial quotation, and guaranteed lead time within 24 hours.
Hot Tags: underground non-rising stem gate valve, China underground non-rising stem gate valve manufacturers, suppliers, factory