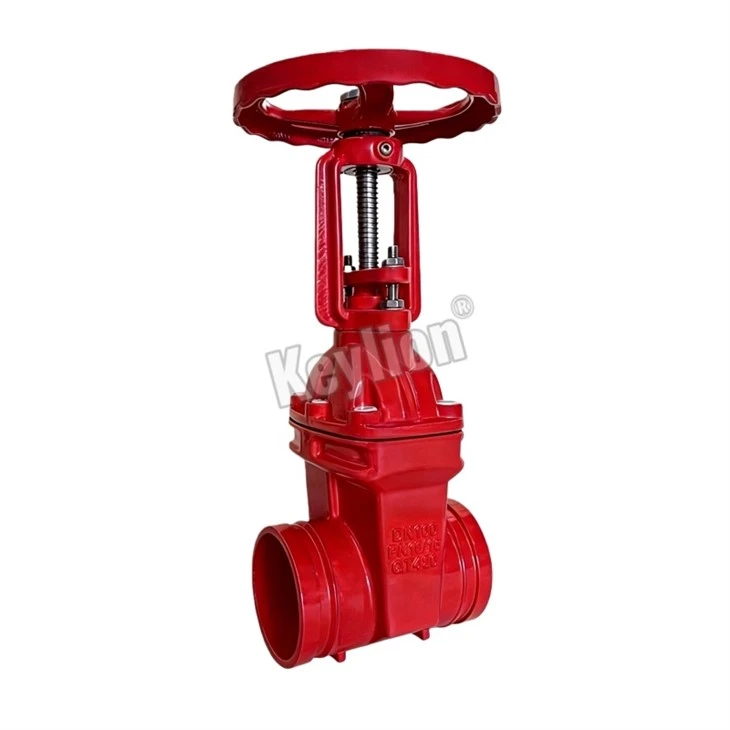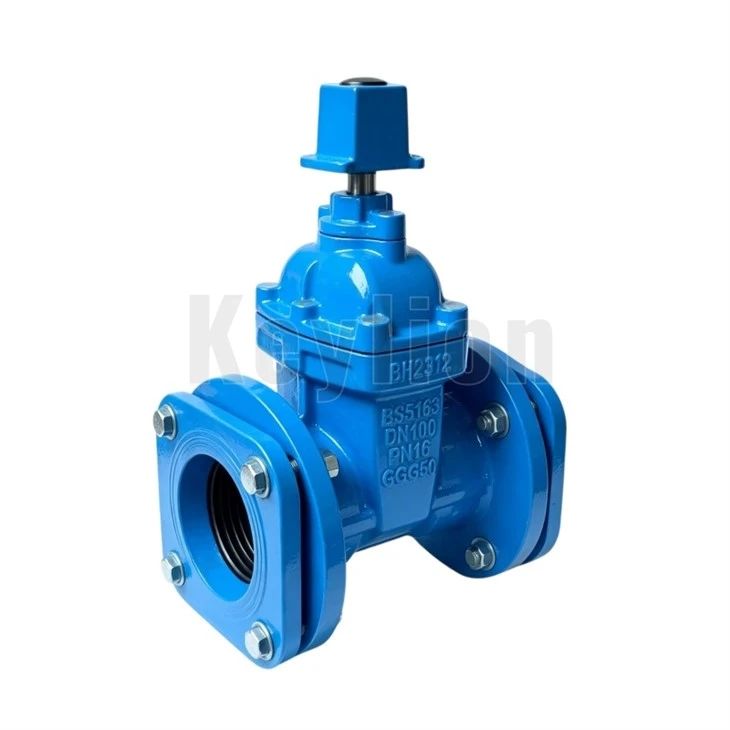
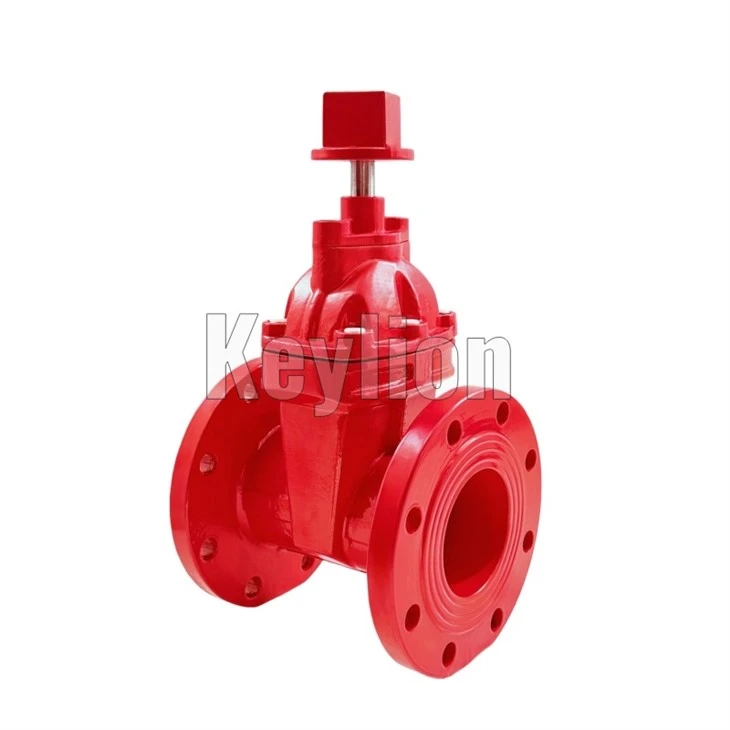
Engineered for buried service in municipal water distribution and underground utility networks, this resilient seated gate valve features a non-rising stem (NRS) mechanism designed to minimize vertical installation clearance. Built with a high-strength ductile iron body and an EPDM/NBR fully encapsulated wedge, it ensures bubble-tight shut-off (Zero Leakage) under working pressures up to PN16 / PN25.
Design & Compliance: Conforms to AWWA C515, BS EN 1074-2, and DIN 3352.
Buried Installation: Optimized for operation via standard 2-inch square nuts, extension spindles, and surface valve boxes.
Corrosion Protection: Fusion Bonded Epoxy (FBE) powder coating applied internally and externally (min. 250 um).
Technical Specifications & Engineering Submittal Assets
|
Parameter |
Specification Details |
|
Size Range |
DN50 - DN600 (2" - 24") |
|
Working Pressure |
PN10, PN16, PN25 (1.0 / 1.6 / 2.5 MPa) |
|
Working Temperature |
-10°C to +80°C (Potable Water) |
|
Body & Bonnet Material |
Ductile Iron (ASTM A536 / GGG50 / EN-GJS-500-7) |
|
Wedge Material |
Ductile Iron core, fully vulcanized with EPDM or NBR |
|
Stem Material |
Stainless Steel (AISI 420 / AISI 316) |
|
Connection Type |
Flanged (EN 1092-2 / ANSI B16.5) or Socket/Mechanical Joint |
|
Coating |
Fusion Bonded Epoxy (FBE) to AWWA C550 / WRAS approved |
Key Features & Manufacturing Integrity
Precision Ductile Iron Casting: Valve bodies and bonnets are produced via resin-bonded sand casting processes using GGG50 material, ensuring high tensile strength (>= 500 MPa) and resistance to pipe stress and ground subsidence.
Fully Encapsulated Wedge: The wedge is uniformly coated with high-grade EPDM elastomer. The vulcanization process guarantees strong rubber-to-metal bonding, preventing fluid contact with the base iron core and eliminating corrosion pitting.
Triple O-Ring Stem Seal: The upper stem features three independent O-ring seals designed to prevent groundwater infiltration and leakage under high operating cycles. Maintenance can be performed under line pressure for specific configurations.
Low Operating Torque: The bronze stem nut is precision-machined with rolled threads, reducing operational friction and allowing smooth actuation via standard T-wrenches or gearbox actuators.
Applications
Municipal Water Distribution: Main isolation valves in underground city water grids.
Fire Protection Systems: Underground fire hydrant supply loops requiring dependable open/shut verification.
Desalination & Water Treatment: Intake pipelines and raw water transfer infrastructure.
Irrigation Networks: Agricultural and district-level bulk water delivery systems.
OEM & Customization Capabilities
Manufacturing Infrastructure: In-house foundry operations, CNC vertical machining centers, and automated electrostatic FBE coating lines control the complete production cycle from raw casting to final assembly.
Custom Tailoring:
Actuation Options: Square operating nut (standard for buried service), ISO 5210 top flange for electric actuators, or handwheel with gearbox.
Stem Extensions: Custom stem lengths manufactured to specific burial depths (1.0m to 3.0m).
Flange Drilling: Custom drilling patterns matching ANSI B16.5, AS 2129, or JIS B2220 standards upon request.
Testing, Quality & Documentation
Every production batch undergoes strict quality verification prior to dispatch:
Pressure Testing: Tested in accordance with EN 12266-1 / API 598.
Shell Test: 1.5 x working pressure.
Seat Test: 1.1 x working pressure (Zero leakage allowed).
Coating Inspection: Wet film and dry film thickness testing (>= 250 um), high-voltage pin-hole holiday test (2.5 kV), and cross-cut adhesion test.
Traceability: Heat numbers cast directly onto body components; Material Test Certificates (EN 10204 3.1) and third-party inspection reports (SGS/BV) provided upon request.
FAQ
Q: What is the standard coating thickness, and is it certified for potable water?
A: The standard FBE coating thickness is minimum 250 um. The powder utilized complies with WRAS and NSF/ANSI 61 standards for direct contact with drinking water.
Q: Can these valves be operated directly when buried underground?
A: Yes. For buried applications, valves are supplied with a standard 2-inch square operating nut, connected to a vertical extension rod housed inside a surface valve box (surface box supplied optionally).
Q: What is your standard delivery lead time for bulk municipal orders?
A: Standard sizes (DN100-DN300) in PN16 execution typically ship within 25 to 35 days from order confirmation. Exact lead times depend on order volume and required testing certificates.
Q: Do you supply third-party inspection reports with shipments?
A: Yes. We routinely facilitate inspections by independent agencies such as SGS, Bureau Veritas, or TÜV prior to final crating.
Request a Project Quotation (RFQ)
To receive an immediate commercial offer, project quotation, or engineering submittal package for your water supply project, please include the following parameters in your inquiry:
Size & Pressure: Nominal Diameter (DN) & Working Pressure (PN)
Standard & Certifications: e.g., AWWA C515, BS 5163, WRAS, NSF 61
Quantity & Destination: Total order volume and target delivery port/job site
[Submit Your RFQ / Connect with an Application Engineer]
Hot Tags: underground gate valve for water supply, China underground gate valve for water supply manufacturers, suppliers, factory